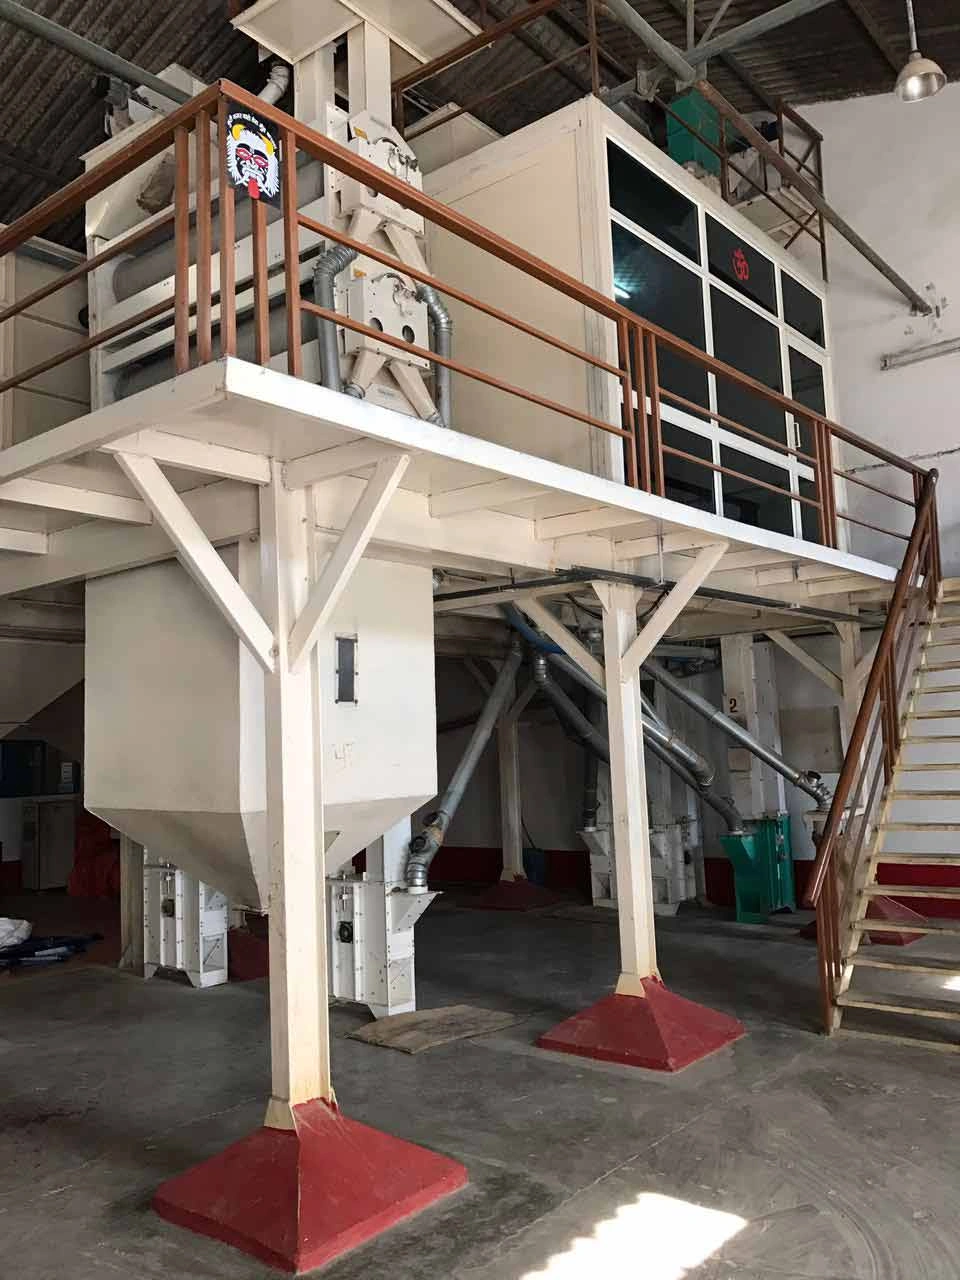
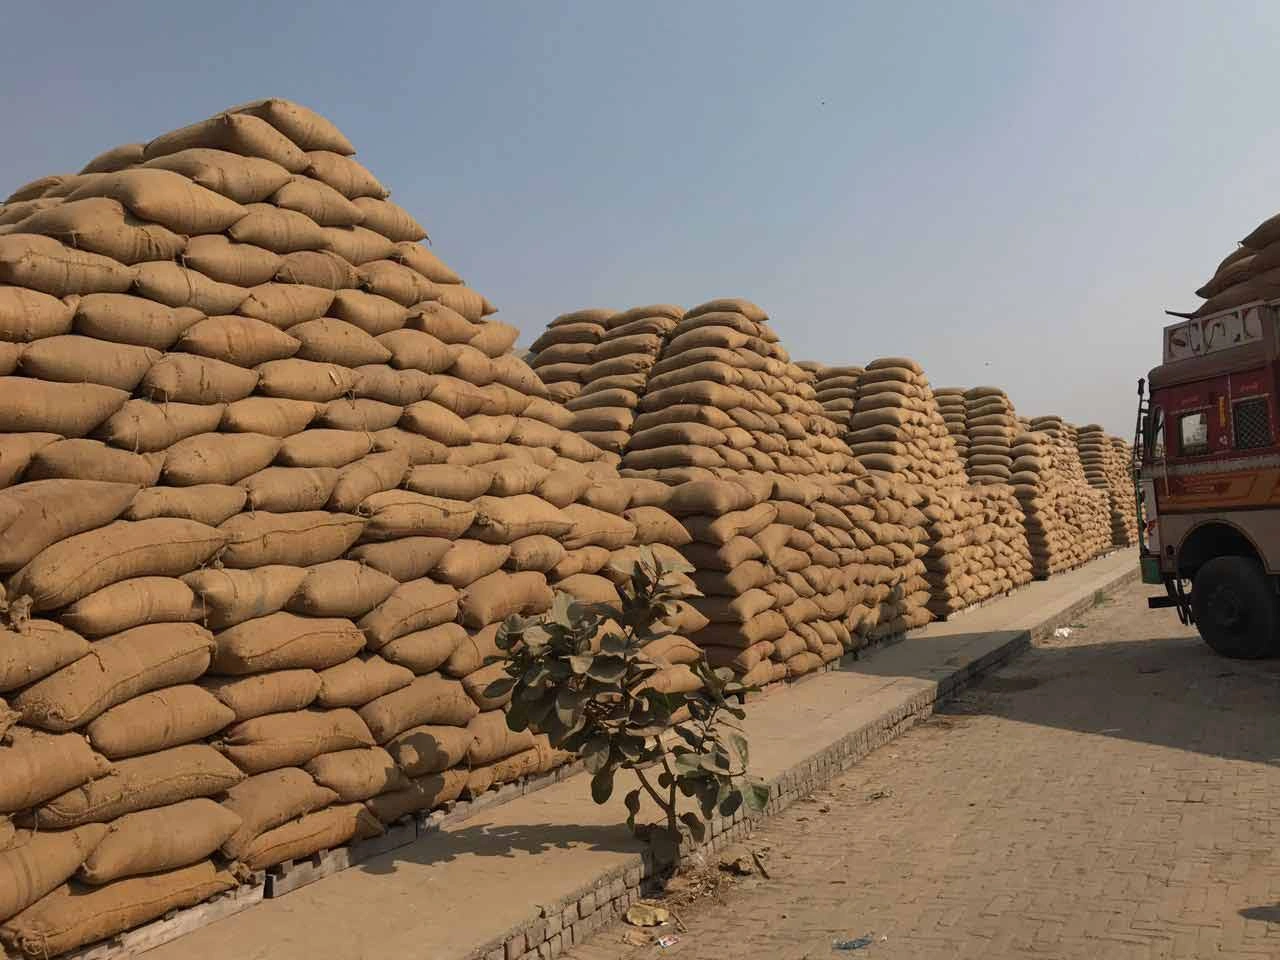
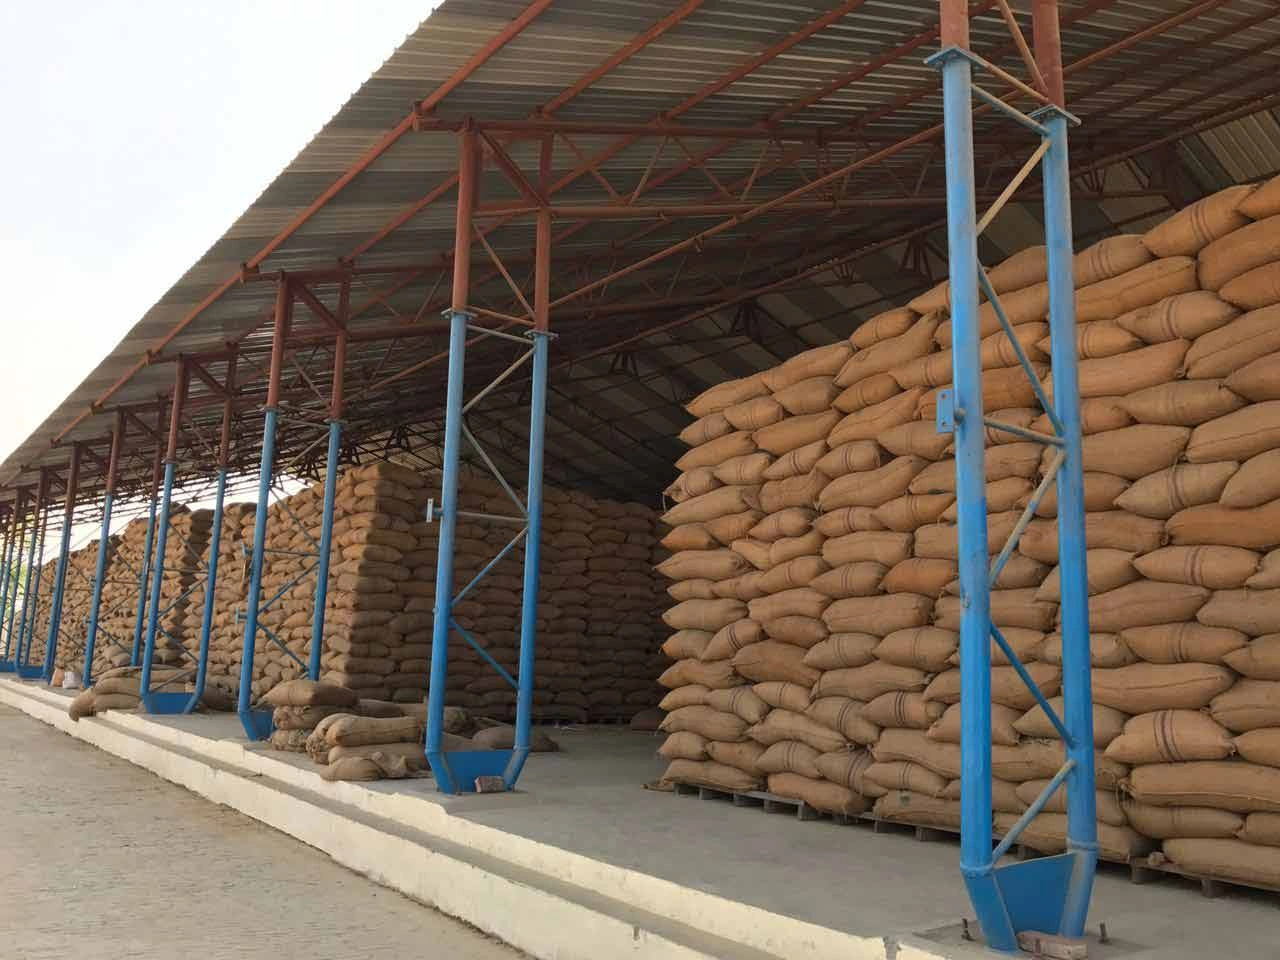
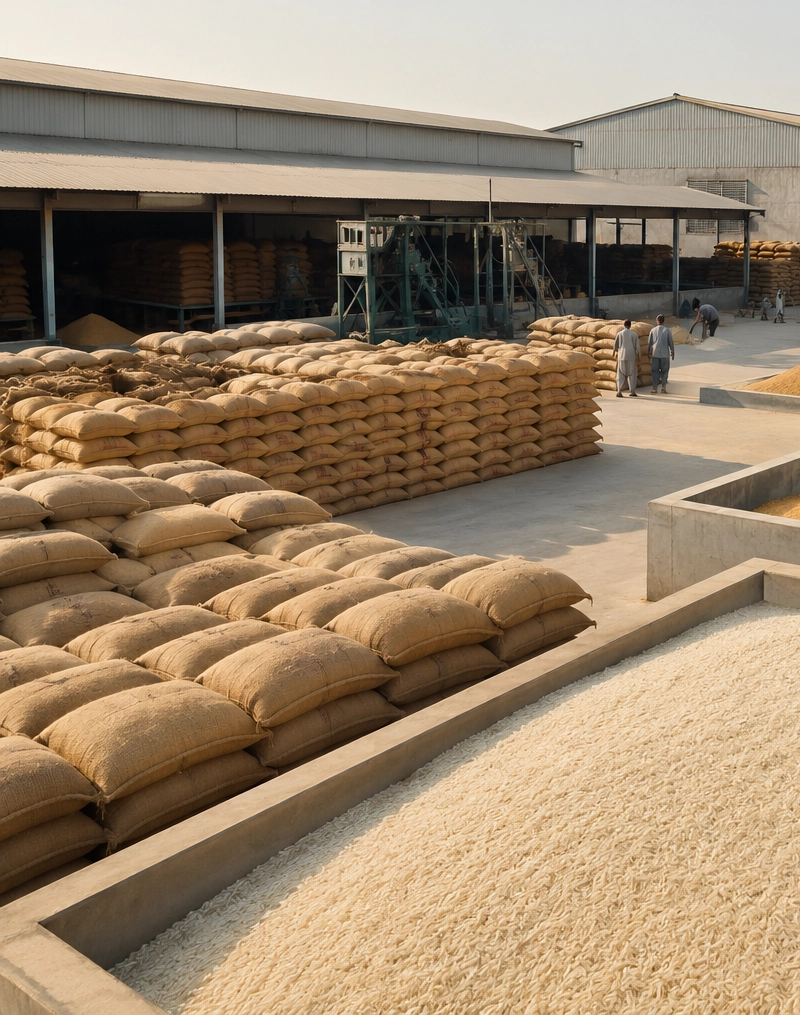
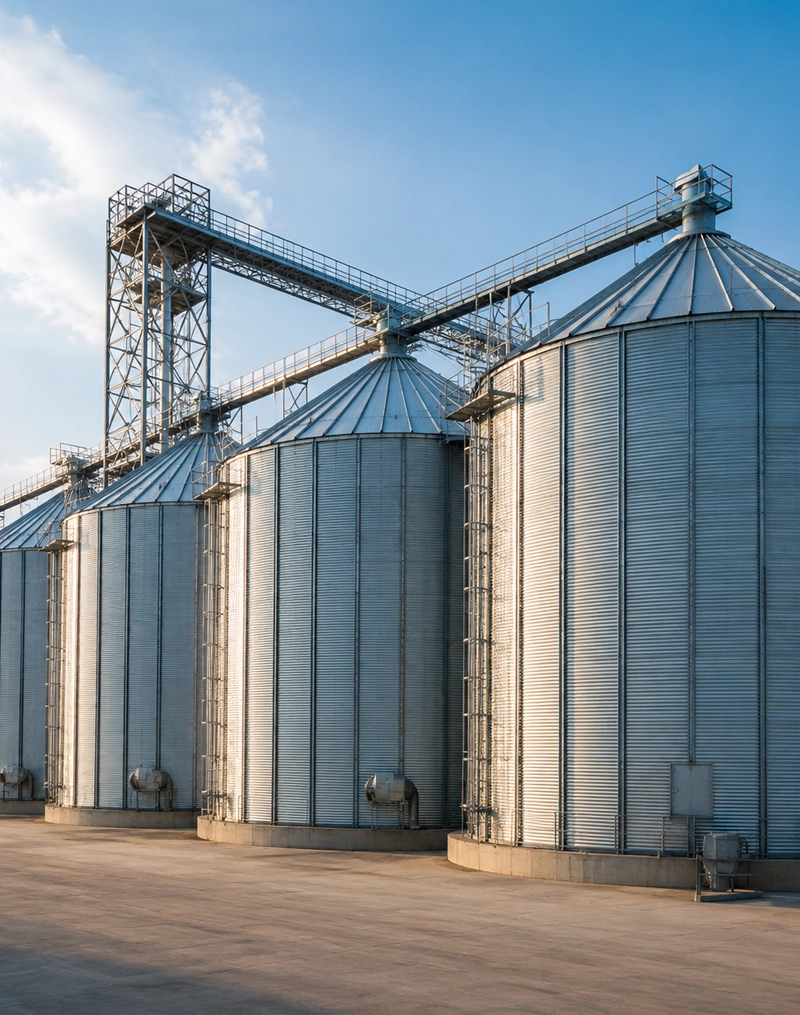
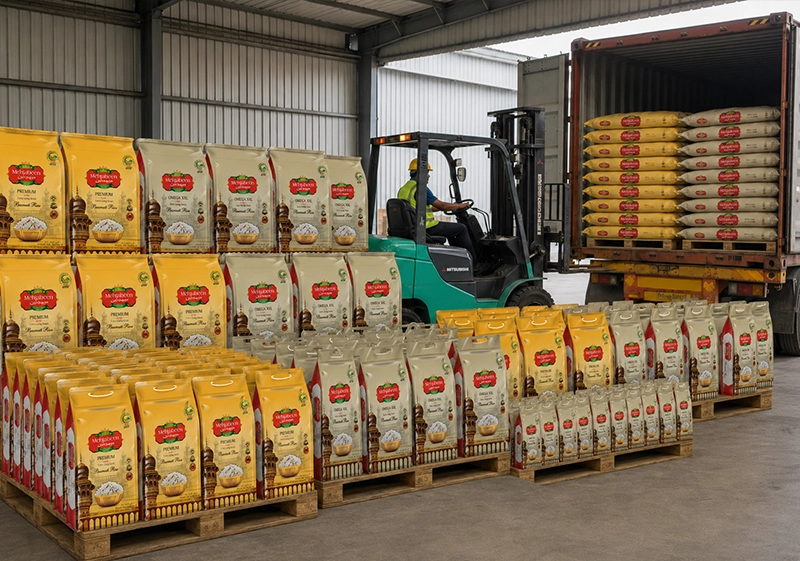
At our Madlauda, Panipat facility, every stage of processing is brought together under one roof — cleaning, milling, grading, packing and loading. This integrated approach gives us the control and capacity to deliver consistent quality at scale, shipment after shipment.
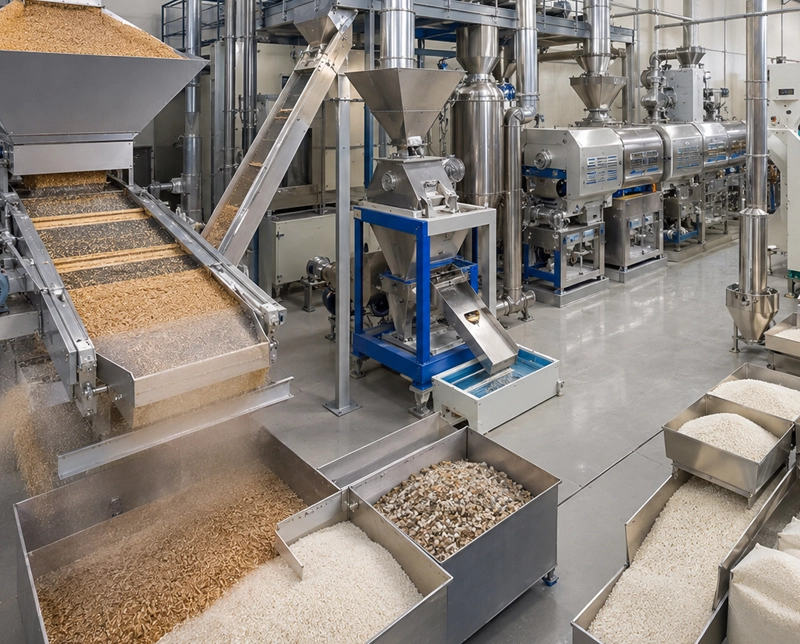
Every batch entering our mill follows the same carefully controlled four-stage process — designed to protect the grain, maintain consistency, and deliver the quality G.R. International stands for.
A Cleaner Start to Every Batch
Incoming paddy undergoes thorough pre-cleaning to remove dust, husk, stones, and other foreign matter preparing the grain for precise milling and ensuring a clean, controlled process from the very first stage.
Removing What Doesn't Belong
Advanced gravity and magnetic separation help remove stones, metal particles, and other unwanted materials before milling ensuring cleaner, safer grain enters the next stage.
Precision in Every Grain
Carefully controlled milling and polishing refine the grain to achieve a clean, consistent finish — maintaining uniformity across every batch and grade.
Consistency You Can See
Each batch is precisely sorted by grain length and colour before packing, helping ensure uniform appearance, quality, and grade consistency in every shipment.
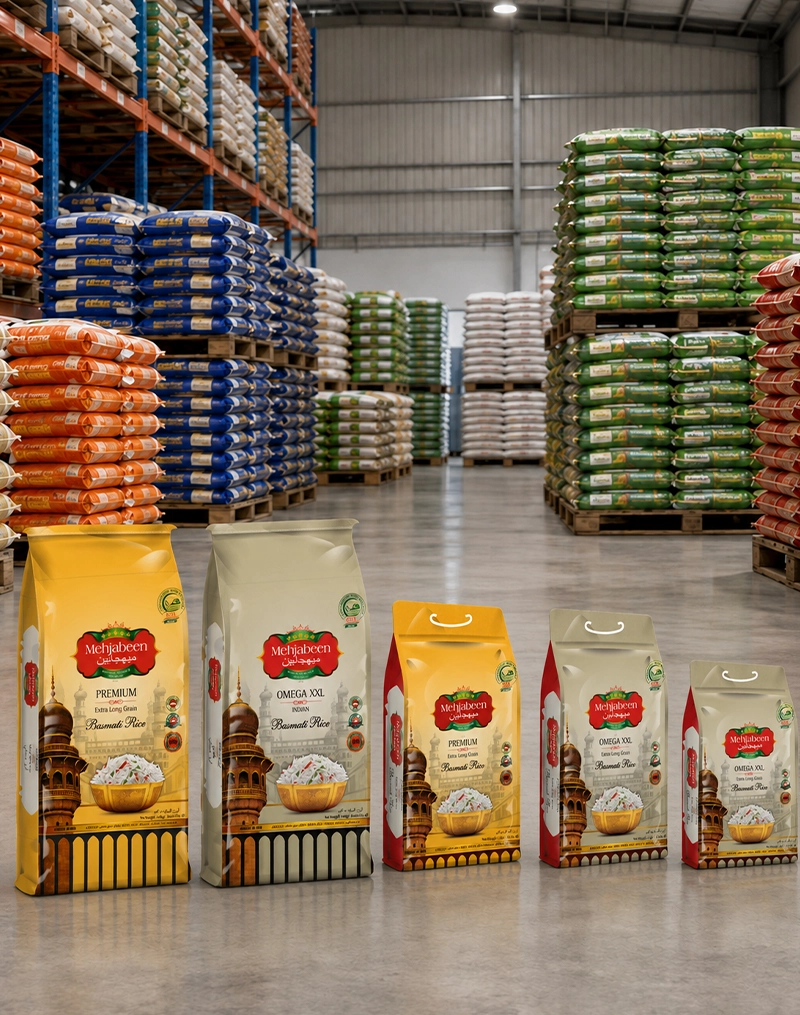
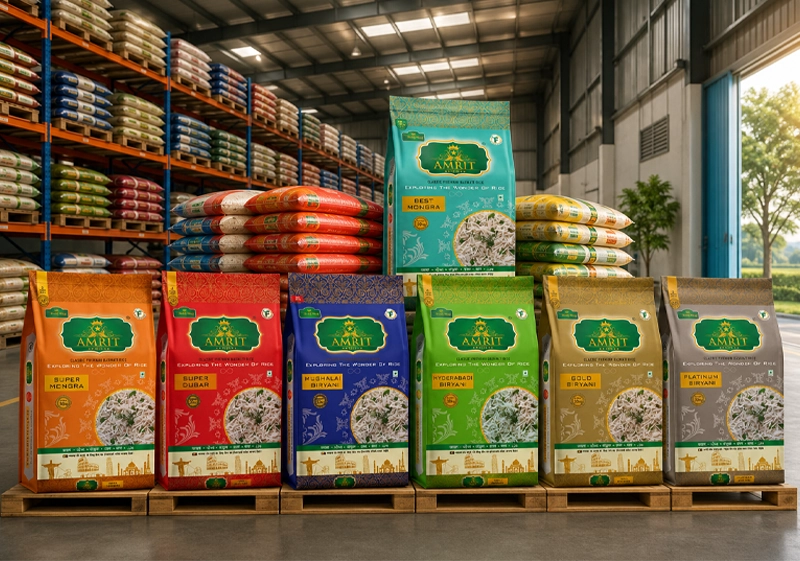
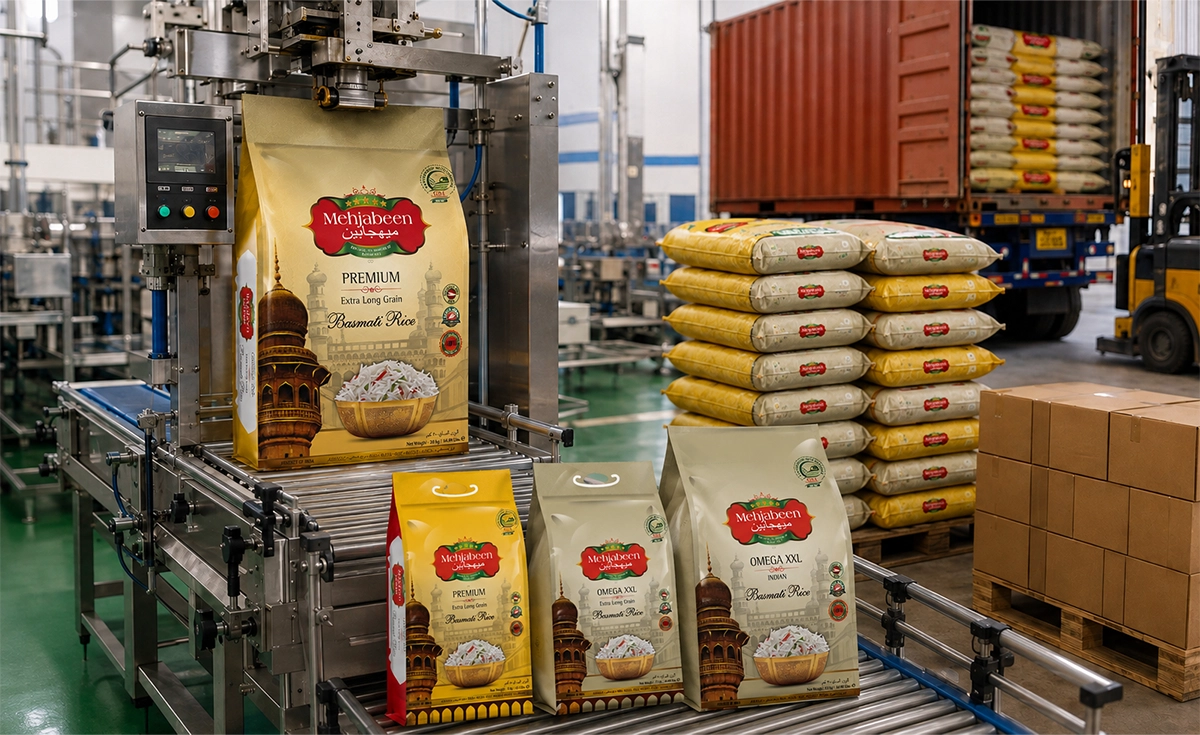
At G.R. International, packaging takes place on the same site as milling, allowing every batch to move directly from grading to final packing under controlled conditions. We offer PP woven and laminated packaging with heat-sealed, moisture resistant closures designed to protect grain quality, aroma, and shelf life throughout long-distance transportation. Private label and multilingual labelling options are also available to meet the requirements of international markets. Every pack is finished with our hologram anti-counterfeit seal, giving buyers an additional way to verify product authenticity before purchase.
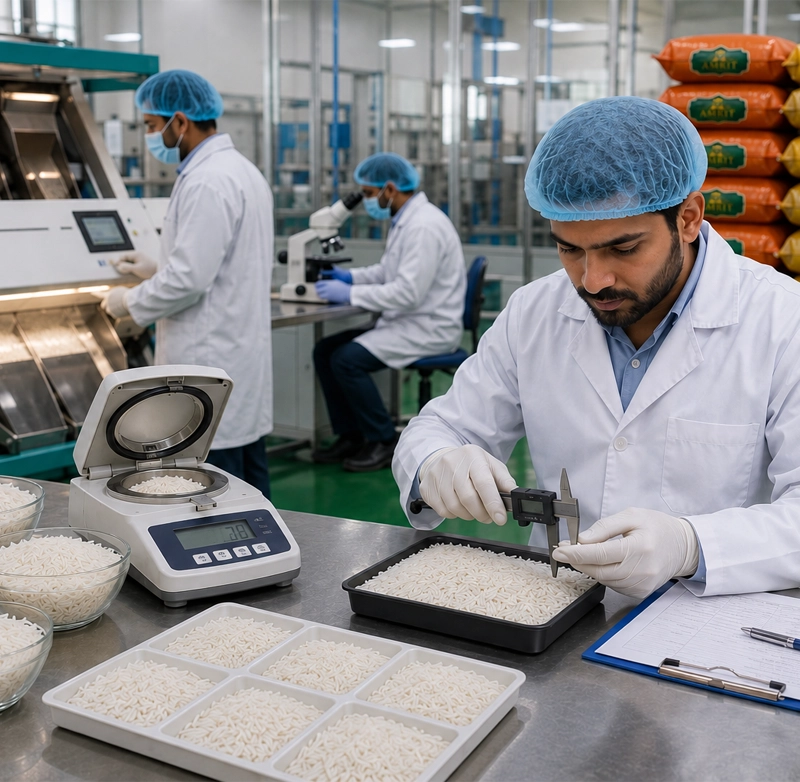
In-house testing at every stage, not just a final inspection before dispatch.
Every lot is checked for moisture content to protect shelf life in transit.
Optical sorting removes discoloured and broken grains from every batch.
Multi stage screening clears dust, husk and non grain material before packing.
Random sampling confirms that the grain length matches the declared grade.
Every batch is logged against its packing date and batch number for traceability.
A final check against buyer specification before any bag leaves the facility.
From controlled aging to bulk storage and final staging, every grain remains within our facility — ensuring quality is preserved and shipments are ready when required.
The final stretch of every shipment is managed in-house — from finished rice and final quality checks to secure loading and container dispatch, ensuring every order leaves our facility ready for its destination.
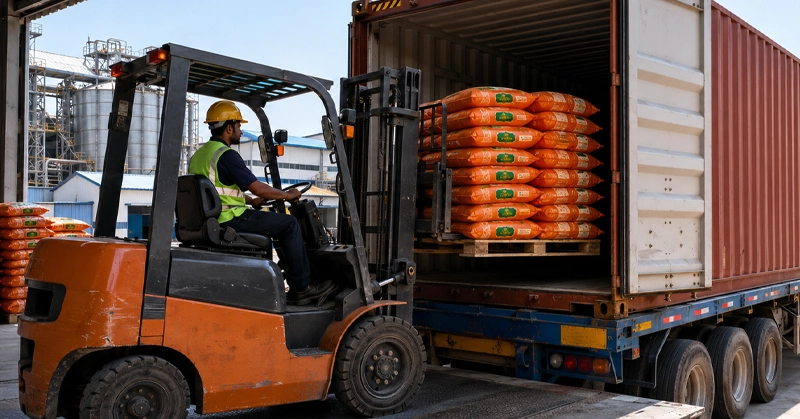
Direct-from-mill container stuffing for FCL shipments, minimising handling between final packing and port dispatch while keeping every consignment secure and export-ready.
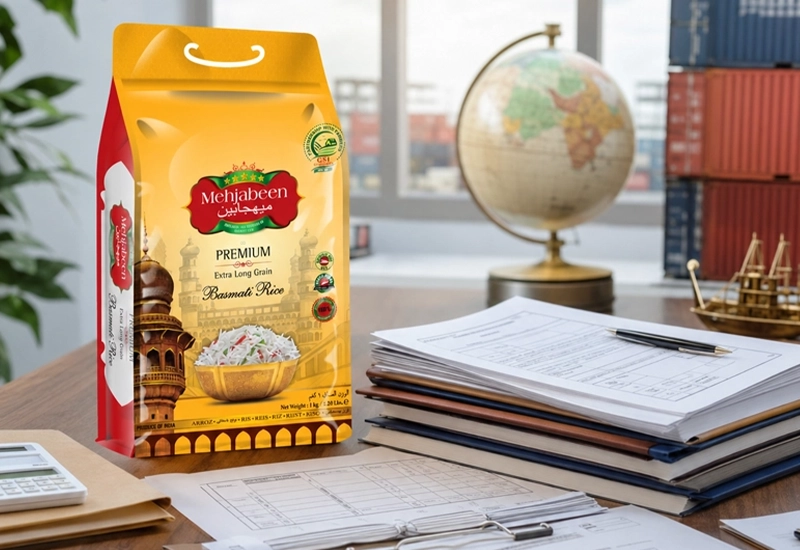
All essential export documents — including invoices, packing lists, certificates of origin and phytosanitary certificates — are prepared in-house for each shipment, ensuring accuracy, compliance and smooth customs clearance.
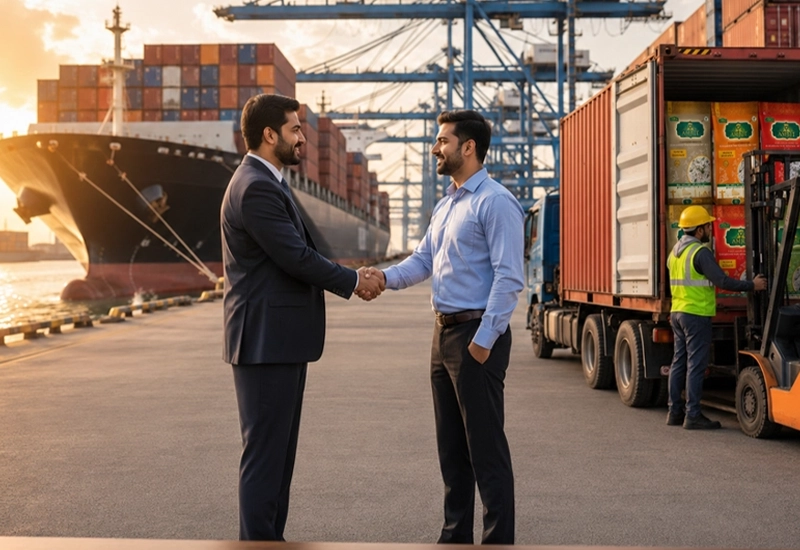
Established relationships with shipping lines and freight forwarders across our core export markets, helping coordinate reliable, efficient movement from our facility to the final destination.
Exploring the wonders of rice since 1989, G.R. International mills, ages and grades Basmati, Non-Basmati and Brown Rice for importers across 50+ countries, from Panipat, Haryana to your table worldwide.